วันอังคารที่ 29 มกราคม พ.ศ. 2562

วันเสาร์ที่ 30 กันยายน พ.ศ. 2560
วันจันทร์ที่ 3 เมษายน พ.ศ. 2560
ก้าวแรกเว็บมาสเตอร์
#ก้าวแรกเว็บมาสเตอร์
#ฟรีโฮส
http://api.hostinger.in.th/redir/2858796
#ฟรีโดเมนเนม
http://www.freenom.com/th/index.html
ลองแล้วดีฟรีทุกอย่าง
http://www.cnc1.tk
วันพุธที่ 17 เมษายน พ.ศ. 2556
โปรแกรม แบบเบาๆ
โปรแกรม แบบเบาๆ
ไม่ง่ายและไม่ยากใช้สมองคนล้วนๆและเครื่องคิดเลขและพิมพ์เองลงเครื่องcnc
START
&HE:%
:2000(QSB-35-STEP 1)
G00G17G49G80G40
G91G28Z0
G91G28Y0
G10G90L2P1X-275.183Y-193.576Z-608.
(-----)
T5M6
T2
N1
M01(FACE 100.0MM)
G54G90G00X-260.Y132.
G43Z100.H5M3S900
Z20.M08
G01Z4.F700
X260.
G00Y50.
G01X-260.
G00Y-35.
G01X260.
G00Y-130.
G01X-260.
G00Y132.
G01Z2.
X260.
G00Y50.
G01X-260.
G00Y-35.
G01X260.
G00Y-130.
G01X-260.
G00Y132.
G01Z0.5
X260.
G00Y50.
G01X-260.
G00Y-35.
G01X260.
G00Y-130.
G01X-260.
G00Y132.
G01Z0.2
X260.
G00Z50.
Y-132.X-260.
G00Z5.
G01Z0.2
G01X260.
G00Z50.
G00Y-39.X-260.
G00Z-1.
G01X260.
G00Y39.
G01X-260.
G00G90Z100.M09
G91G28Z0M5
G91G28Y0
(----)
T2M6
T17
N2
M01(INSERT=32)
G54G90G00X-221.Y-74.
G43Z100.H02M3S1700
Z5.M08
G01Z-1.F700
X221.
G00Y74.
G01X-221.
G00Z50.
X9.Y-188.
Z-1.
G01Y-74.
X-9.
Y-188.
G00X91.
G01Y-74.
X109.
Y-188.
G00X-91.
G01Y-74.
X-109.
Y-188.
G00Z50.
Y188.X-109.
Z-1.
G01Y74.
X-91.
Y188.
G00X9.Y188.
G01Y74.
X-9.
Y188.
G00X91.
G01Y74.
X109.
Y188.
G00Z50.
X222.Y0
G01Z-3.F2000
M98P2009
Z-6.
M98P2009
Z-9.
M98P2009
Z-12.
M98P2009
Z-15.
M98P2009
Z-18.
M98P2009
Z-21.
M98P2009
Z-24.
M98P2009
Z-27.
M98P2009
Z-30.
M98P2009
G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(------)
T17M6
T3
N3
M01(ENDMILL=20)
G54G90G00X220.Y0
G43Z100.H27M3S1100
Z5.M08
G01Z-28.F2000
G41G01X190.D28
Y-152.5F300
Y-157.45X185.
X-185.
X-190.Y-152.5
Y152.5
Y157.45X-185.
X185.
X190.Y152.5
Y0
G40X220.Y0
G00Z50.
X0Y-40.
Z5.
G01Z-4.F2000
M98P2011
Z-7.
M98P2011
Z-10.
M98P2011
Z-13.
M98P2011
Z-16.
M98P2011
Z-19.
M98P2011
Z-21.5
M98P2011
Z-24.
M98P2011
Z-27.
M98P2011
Z-30.
M98P2011
G01Z-29.9F300
Y-55.
X60.
Y55.
X-60.
Y-55.
X0
Y-40.
G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(-------)
T3M6
T9
N4
M01(CENTERDRILL)
G54G90G00X0Y0
G43Z100.H03M3S1700
M08
G81G99Z-4.R5.F200
M98P2012
M98P2013
G80G90G00Z100.M9
G91G28Z0M5
G91G28Y0
(------)
T9M6
T13
N5
M01(DRILL=5)
G54G90G00X0Y110.
G43Z100.H09M03S1500
M08
G83G99Z-30.R5.F130.Q5.
Y-110.
G80G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(--------)
T13M6
T10
N6
M01(DRILL 7.0MM)
G54G90G00X95.Y32.5
G43Z100.H13M3S1400
M08
G83G99Z-53.R4.Q5.F140.
M98P2006
G80G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(------)
T10M6
T12
N7
M01(DRILL=11)
G54G90G00X95.Y32.5
G43Z100.H29M3S950
M08
G83G99Z-29.5R4.F120.Q5.
M98P2006
X150.Y110.Z-10.5
M98P2008
G80G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(--------)
T12M6
T4
N8
M01(ENDMILL=11)
G54G90G00X95.Y32.5
G43Z100.H12M3S900
M08
G82G99Z-29.5R4.F90P500
M98P2006
G80G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(-------)
T4M6
T15
N9
M01(DRILL=9)
G54G90G00X150.Y110.
G43Z100.H4M3S860
M08
G83G99Z-32.R5.F130Q5.
M98P2008
M98P2005
G80G90G00Z100.M9
G91G28Z0M5
G91G28Y0
(-------)
T15M6
T6
N10
M01(ENDMILL=14)
G54G90G00X150.Y110.
G43Z100.H15M3S1200
M08
G82G99Z-10.R5.F80P500
M98P2008
G80G90G00Z100.M9
G91G28Z0M5
G91G28Y0
(------)
T6M6
T14
N11
M01(DRILL 9.8)
G54G90X-142.5Y0
G43Z100.H6M3S900
M08
G83G98Z-21.R5.F100Q5.
G80G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(-------)
T14M6
T16
N12
M01(REAMER=10)
G54G90G00X-142.5Y0
G43Z100.H14M3S300
M08
G85G98Z-16.R5.F96
G80G90G00Z100.M9
G91G28Z0M5
G91G28Y0
(--------)
T16M6
N13
M01(CHAMFER)
G54G90G0X-142.5Y0
G43Z100.H16M3S2200
M08
G82G99Z-4.2R5.F300P500
X95.Y32.5Z-4.6
M98P2006
X150.Y110.Z-5.2
M98P2008
X150.Y140.Z-2.4
X50.
X-50.
X-150.
Y-140.
X-50.
X50.
X150.
G80G90G00Z30.
X0Y-50.
G01Z-9.5F2000
Y-55.F500
X60.
Y55.
X-60.
Y-55.
X0
G00Z20.
X215.Y0
Z-5.5
G41G01X190.D08F1000
Y-152.5
Y-157.5X185.
X-185.
X-190.Y-152.5
Y152.5
Y157.5X-185.
X185.
X190.Y152.5
Y0
G40G01Y0X215.
G00Z50.
X220.Y88.
Z-6.
G01X197.F1000
Y-88.
X220.
G00Y-177.
X123.
G01Y-164.5
X77.
Y-177.
X23.G00
G01Y-164.5
X-23.
Y-177.
G00X-77.
G01Y-164.5
X-123.
Y-177.
G00X-220.
Y-88.
G01X-197.
Y88.
X-220.
G00Y177.
X-123.
G01Y164.5
X-77.
Y177.
G00X-23.
G01Y164.5
X23.
Y177.
G00X77.
G01Y164.5
X123.
Y177.
G40G90G00Z100.M9
G91G28Z0M5
G91G28Y0
(-------)
T0M6
G90X0
M30
%
ไม่ง่ายและไม่ยากใช้สมองคนล้วนๆและเครื่องคิดเลขและพิมพ์เองลงเครื่องcnc
START
&HE:%
:2000(QSB-35-STEP 1)
G00G17G49G80G40
G91G28Z0
G91G28Y0
G10G90L2P1X-275.183Y-193.576Z-608.
(-----)
T5M6
T2
N1
M01(FACE 100.0MM)
G54G90G00X-260.Y132.
G43Z100.H5M3S900
Z20.M08
G01Z4.F700
X260.
G00Y50.
G01X-260.
G00Y-35.
G01X260.
G00Y-130.
G01X-260.
G00Y132.
G01Z2.
X260.
G00Y50.
G01X-260.
G00Y-35.
G01X260.
G00Y-130.
G01X-260.
G00Y132.
G01Z0.5
X260.
G00Y50.
G01X-260.
G00Y-35.
G01X260.
G00Y-130.
G01X-260.
G00Y132.
G01Z0.2
X260.
G00Z50.
Y-132.X-260.
G00Z5.
G01Z0.2
G01X260.
G00Z50.
G00Y-39.X-260.
G00Z-1.
G01X260.
G00Y39.
G01X-260.
G00G90Z100.M09
G91G28Z0M5
G91G28Y0
(----)
T2M6
T17
N2
M01(INSERT=32)
G54G90G00X-221.Y-74.
G43Z100.H02M3S1700
Z5.M08
G01Z-1.F700
X221.
G00Y74.
G01X-221.
G00Z50.
X9.Y-188.
Z-1.
G01Y-74.
X-9.
Y-188.
G00X91.
G01Y-74.
X109.
Y-188.
G00X-91.
G01Y-74.
X-109.
Y-188.
G00Z50.
Y188.X-109.
Z-1.
G01Y74.
X-91.
Y188.
G00X9.Y188.
G01Y74.
X-9.
Y188.
G00X91.
G01Y74.
X109.
Y188.
G00Z50.
X222.Y0
G01Z-3.F2000
M98P2009
Z-6.
M98P2009
Z-9.
M98P2009
Z-12.
M98P2009
Z-15.
M98P2009
Z-18.
M98P2009
Z-21.
M98P2009
Z-24.
M98P2009
Z-27.
M98P2009
Z-30.
M98P2009
G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(------)
T17M6
T3
N3
M01(ENDMILL=20)
G54G90G00X220.Y0
G43Z100.H27M3S1100
Z5.M08
G01Z-28.F2000
G41G01X190.D28
Y-152.5F300
Y-157.45X185.
X-185.
X-190.Y-152.5
Y152.5
Y157.45X-185.
X185.
X190.Y152.5
Y0
G40X220.Y0
G00Z50.
X0Y-40.
Z5.
G01Z-4.F2000
M98P2011
Z-7.
M98P2011
Z-10.
M98P2011
Z-13.
M98P2011
Z-16.
M98P2011
Z-19.
M98P2011
Z-21.5
M98P2011
Z-24.
M98P2011
Z-27.
M98P2011
Z-30.
M98P2011
G01Z-29.9F300
Y-55.
X60.
Y55.
X-60.
Y-55.
X0
Y-40.
G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(-------)
T3M6
T9
N4
M01(CENTERDRILL)
G54G90G00X0Y0
G43Z100.H03M3S1700
M08
G81G99Z-4.R5.F200
M98P2012
M98P2013
G80G90G00Z100.M9
G91G28Z0M5
G91G28Y0
(------)
T9M6
T13
N5
M01(DRILL=5)
G54G90G00X0Y110.
G43Z100.H09M03S1500
M08
G83G99Z-30.R5.F130.Q5.
Y-110.
G80G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(--------)
T13M6
T10
N6
M01(DRILL 7.0MM)
G54G90G00X95.Y32.5
G43Z100.H13M3S1400
M08
G83G99Z-53.R4.Q5.F140.
M98P2006
G80G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(------)
T10M6
T12
N7
M01(DRILL=11)
G54G90G00X95.Y32.5
G43Z100.H29M3S950
M08
G83G99Z-29.5R4.F120.Q5.
M98P2006
X150.Y110.Z-10.5
M98P2008
G80G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(--------)
T12M6
T4
N8
M01(ENDMILL=11)
G54G90G00X95.Y32.5
G43Z100.H12M3S900
M08
G82G99Z-29.5R4.F90P500
M98P2006
G80G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(-------)
T4M6
T15
N9
M01(DRILL=9)
G54G90G00X150.Y110.
G43Z100.H4M3S860
M08
G83G99Z-32.R5.F130Q5.
M98P2008
M98P2005
G80G90G00Z100.M9
G91G28Z0M5
G91G28Y0
(-------)
T15M6
T6
N10
M01(ENDMILL=14)
G54G90G00X150.Y110.
G43Z100.H15M3S1200
M08
G82G99Z-10.R5.F80P500
M98P2008
G80G90G00Z100.M9
G91G28Z0M5
G91G28Y0
(------)
T6M6
T14
N11
M01(DRILL 9.8)
G54G90X-142.5Y0
G43Z100.H6M3S900
M08
G83G98Z-21.R5.F100Q5.
G80G90G00Z100.M09
G91G28Z0M5
G91G28Y0
(-------)
T14M6
T16
N12
M01(REAMER=10)
G54G90G00X-142.5Y0
G43Z100.H14M3S300
M08
G85G98Z-16.R5.F96
G80G90G00Z100.M9
G91G28Z0M5
G91G28Y0
(--------)
T16M6
N13
M01(CHAMFER)
G54G90G0X-142.5Y0
G43Z100.H16M3S2200
M08
G82G99Z-4.2R5.F300P500
X95.Y32.5Z-4.6
M98P2006
X150.Y110.Z-5.2
M98P2008
X150.Y140.Z-2.4
X50.
X-50.
X-150.
Y-140.
X-50.
X50.
X150.
G80G90G00Z30.
X0Y-50.
G01Z-9.5F2000
Y-55.F500
X60.
Y55.
X-60.
Y-55.
X0
G00Z20.
X215.Y0
Z-5.5
G41G01X190.D08F1000
Y-152.5
Y-157.5X185.
X-185.
X-190.Y-152.5
Y152.5
Y157.5X-185.
X185.
X190.Y152.5
Y0
G40G01Y0X215.
G00Z50.
X220.Y88.
Z-6.
G01X197.F1000
Y-88.
X220.
G00Y-177.
X123.
G01Y-164.5
X77.
Y-177.
X23.G00
G01Y-164.5
X-23.
Y-177.
G00X-77.
G01Y-164.5
X-123.
Y-177.
G00X-220.
Y-88.
G01X-197.
Y88.
X-220.
G00Y177.
X-123.
G01Y164.5
X-77.
Y177.
G00X-23.
G01Y164.5
X23.
Y177.
G00X77.
G01Y164.5
X123.
Y177.
G40G90G00Z100.M9
G91G28Z0M5
G91G28Y0
(-------)
T0M6
G90X0
M30
%
โปรแกรมขั้นเทพ MACRO PROGRAM
โปรแกรมขั้นเทพ MACRO PROGRAM
สำหรับหา FIXTURE ของเครื่อง HORIZONTAL เครื่องกัดแนวนอน
โดยการใส่ค่า x y z ของชิ้นงานเพียงด้านเดียว จะคำนวณออกมาให้3ด้านเลย
โดยโปรแกมจะนำค่าที่ใด้ไปใส่ใน ค่าG54 G55 G56 ให้โดยอัตโนมัติ
โดยใช้ G65 เป็นตัวกำกับ
%001
(MACRO PROGRAM)
#1 EQ #24
#2 EQ #26
#3 EQ #25
#4=0
(G54)
#10=345.
#11=-800.
IF[[#1]GT[#10]]GOTO1
#21=ABS[#10]-ABS[#1]
GOTO2
N1 #21=ABS[ABS[#1]-ABS[#10]]
GOTO2
N2 IF[[#2]GT[#11]]GOTO3
#23=ABS[#11]-ABS[#2]
GOTO10
N3 #23=ABS[ABS[#2]-ABS[#11]]
GOTO10
N10 #24=[#21]*COS[#4]-[#23]*SIN[#4]
#26=[#21]*SIN[#4]+[#23]*COS[#4]
#2501=[#24]+[#10]
#2601=[#3]
#2701=[#26]+[#11]
(G55)
#4=90.
#10=345.
#11=-800.
IF[[#1]GT[#10]]GOTO1
#21=ABS[#10]-ABS[#1]
GOTO2
N1 #21=ABS[ABS[#1]-ABS[#10]]
GOTO2
N2 IF[[#2]GT[#11]]GOTO3
#23=ABS[#11]-ABS[#2]
GOTO10
N3 #23=ABS[ABS[#2]-ABS[#11]]
GOTO10
N10 #24=[#21]*COS[#4]-[#23]*SIN[#4]
#26=[#21]*SIN[#4]+[#23]*COS[#4]
#2502=[#24]+[#10]
#2602=[#3]
#2702=[#26]+[#11]
(G56)
#4=270.
#10=345.
#11=-800.
IF[[#1]GT[#10]]GOTO1
#21=ABS[#10]-ABS[#1]
GOTO2
N1 #21=ABS[ABS[#1]-ABS[#10]]
GOTO2
N2 IF[[#2]GT[#11]]GOTO3
#23=ABS[#11]-ABS[#2]
GOTO10
N3 #23=ABS[ABS[#2]-ABS[#11]]
GOTO10
N10 #24=[#21]*COS[#4]-[#23]*SIN[#4]
#26=[#21]*SIN[#4]+[#23]*COS[#4]
#2503=[#24]+[#10]
#2503=[#3]
#2703=[#26]+[#11]
M99
สำหรับหา FIXTURE ของเครื่อง HORIZONTAL เครื่องกัดแนวนอน
โดยการใส่ค่า x y z ของชิ้นงานเพียงด้านเดียว จะคำนวณออกมาให้3ด้านเลย
โดยโปรแกมจะนำค่าที่ใด้ไปใส่ใน ค่าG54 G55 G56 ให้โดยอัตโนมัติ
โดยใช้ G65 เป็นตัวกำกับ
%001
(MACRO PROGRAM)
#1 EQ #24
#2 EQ #26
#3 EQ #25
#4=0
(G54)
#10=345.
#11=-800.
IF[[#1]GT[#10]]GOTO1
#21=ABS[#10]-ABS[#1]
GOTO2
N1 #21=ABS[ABS[#1]-ABS[#10]]
GOTO2
N2 IF[[#2]GT[#11]]GOTO3
#23=ABS[#11]-ABS[#2]
GOTO10
N3 #23=ABS[ABS[#2]-ABS[#11]]
GOTO10
N10 #24=[#21]*COS[#4]-[#23]*SIN[#4]
#26=[#21]*SIN[#4]+[#23]*COS[#4]
#2501=[#24]+[#10]
#2601=[#3]
#2701=[#26]+[#11]
(G55)
#4=90.
#10=345.
#11=-800.
IF[[#1]GT[#10]]GOTO1
#21=ABS[#10]-ABS[#1]
GOTO2
N1 #21=ABS[ABS[#1]-ABS[#10]]
GOTO2
N2 IF[[#2]GT[#11]]GOTO3
#23=ABS[#11]-ABS[#2]
GOTO10
N3 #23=ABS[ABS[#2]-ABS[#11]]
GOTO10
N10 #24=[#21]*COS[#4]-[#23]*SIN[#4]
#26=[#21]*SIN[#4]+[#23]*COS[#4]
#2502=[#24]+[#10]
#2602=[#3]
#2702=[#26]+[#11]
(G56)
#4=270.
#10=345.
#11=-800.
IF[[#1]GT[#10]]GOTO1
#21=ABS[#10]-ABS[#1]
GOTO2
N1 #21=ABS[ABS[#1]-ABS[#10]]
GOTO2
N2 IF[[#2]GT[#11]]GOTO3
#23=ABS[#11]-ABS[#2]
GOTO10
N3 #23=ABS[ABS[#2]-ABS[#11]]
GOTO10
N10 #24=[#21]*COS[#4]-[#23]*SIN[#4]
#26=[#21]*SIN[#4]+[#23]*COS[#4]
#2503=[#24]+[#10]
#2503=[#3]
#2703=[#26]+[#11]
M99
วันเสาร์ที่ 6 เมษายน พ.ศ. 2556


ส่วนต่างๆของ CONTROL LAYOUT
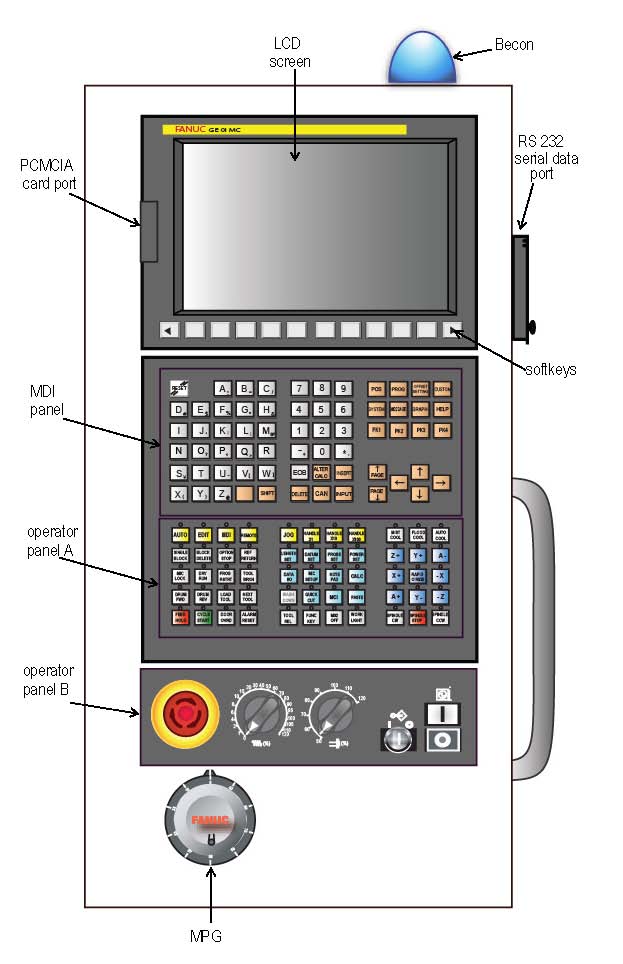
1.RS 232 (ที่เสียบสายRS 232)
2.LCD screen
3.serial data port
4.softkeys(กดเลือกตามที่ขึ้นที่จอ (เหมือนโทรศัพท์))
5.PCMCIA card port
6.MDI panel(ปุ่มกดแก้โปรแกรม)
7.operator panel A
8.operator panel B
9.MPG handle (มือหมุนในโหมดแมนวล)
10.Becon (ไฟสัญญาณ)
------------------------------------------------------------------------------------------------------------

softkeys(กดเลือกตามที่ขึ้นที่จอ (เหมือนโทรศัพท์))
------------------------------------------------------------------------------------------------------------

MDI panel(ปุ่มกดแก้โปรแกรม)
-------------------------------------------------------------------------------------------------------------

operator panel A
------------------------------------------------------------------------------------------------------------

วันเสาร์ที่ 30 มีนาคม พ.ศ. 2556
G04- Dwell, Exact stop --หยุดชั่วขณะเวลา
G04- Dwell, Exact stop --หยุดชั่วขณะเวลา
By specifying a dwell, the execution of the next block is delayed by the
specified time. In addition, a dwell can be specified to make an exact
check in the cutting mode (G64 mode).
When neither P nor X is specified, exact stop is performed.
Bit 1 (DWL) of parameter No. 3405 can specify dwell for each rotation
in feed per rotation mode (G95).
Dwell G04 X_ ; or G04 P_ ;
X_ : Specify a time or spindle speed (decimal point permitted)
P_ : Specify a time or spindle speed (decimal point not permitted)
คำสั่ง G04 X__=0.001 to 99999.999 วินาที or rev
คำสั่ง G04 P__=1 to 99999999 -------0.001 วินาที or rev
EXAMPLE:
ex1.
G01 Z-5 F300 (เดินลงแกน z-5 300mm/นาที)
GO4 X1 (หยูดชั่วขณะ 1วินาที)
หรือ
G01 Z-5 F300 (เดินลงแกน z-5 300mm/นาที)
GO4 P1 (หยูดชั่วขณะ 0.001วินาที)
By specifying a dwell, the execution of the next block is delayed by the
specified time. In addition, a dwell can be specified to make an exact
check in the cutting mode (G64 mode).
When neither P nor X is specified, exact stop is performed.
Bit 1 (DWL) of parameter No. 3405 can specify dwell for each rotation
in feed per rotation mode (G95).
Dwell G04 X_ ; or G04 P_ ;
X_ : Specify a time or spindle speed (decimal point permitted)
P_ : Specify a time or spindle speed (decimal point not permitted)
คำสั่ง G04 X__=0.001 to 99999.999 วินาที or rev
คำสั่ง G04 P__=1 to 99999999 -------0.001 วินาที or rev
EXAMPLE:
ex1.
G01 Z-5 F300 (เดินลงแกน z-5 300mm/นาที)
GO4 X1 (หยูดชั่วขณะ 1วินาที)
หรือ
G01 Z-5 F300 (เดินลงแกน z-5 300mm/นาที)
GO4 P1 (หยูดชั่วขณะ 0.001วินาที)
G03- Circular interpolation
G03- Circular interpolation/Helical interpolation Counterclockwise
G3 is used for CCW circular interpolation and helical moves
G03 เดินวงกลมในทิศทางทวนเข็มนาฬิกา โดยใช้คู่กับ I,J,,R
I : แกนX coordinate of the vector from the start point to the center
J : แกนY coordinate of the vector from the start point to the center
R : รัศมี Radius at the beginning of spiral interpolation
EXAMPLE:
ex1.
G03 X1. Y1. I-1. J0
ex2.
G91 G03 XP60.0 YP20.0 R50.0 F300.0 ;
G91 G03 XP60.0 YP20.0 R–50.0 F300.
G3 is used for CCW circular interpolation and helical moves
G03 เดินวงกลมในทิศทางทวนเข็มนาฬิกา โดยใช้คู่กับ I,J,,R
I : แกนX coordinate of the vector from the start point to the center
J : แกนY coordinate of the vector from the start point to the center
R : รัศมี Radius at the beginning of spiral interpolation
EXAMPLE:
ex1.
G03 X1. Y1. I-1. J0
ex2.
G91 G03 XP60.0 YP20.0 R50.0 F300.0 ;
G91 G03 XP60.0 YP20.0 R–50.0 F300.
G02- Circular interpolation
G02- Circular interpolation/Helical interpolation Clockwise
The command below will move a tool along a circular arc.Clockwise
G02 is used for CW circular interpolation and helical moves.
G02 เดินวงกลมในทิศทางตามเข็มนาฬิกา โดยใช้คู่กับ I,J,,R
I : แกนX coordinate of the vector from the start point to the center
J : แกนY coordinate of the vector from the start point to the center
R : รัศมี Radius at the beginning of spiral interpolation
EXAMPLE:
ex1.
G02 X1. Y1. I-1. J0
ex2.
G91 G02 XP60.0 YP20.0 R50.0 F300.0 ;
G91 G02 XP60.0 YP20.0 R–50.0 F300.
The command below will move a tool along a circular arc.Clockwise
G02 is used for CW circular interpolation and helical moves.
G02 เดินวงกลมในทิศทางตามเข็มนาฬิกา โดยใช้คู่กับ I,J,,R
I : แกนX coordinate of the vector from the start point to the center
J : แกนY coordinate of the vector from the start point to the center
R : รัศมี Radius at the beginning of spiral interpolation
EXAMPLE:
ex1.
G02 X1. Y1. I-1. J0
ex2.
G91 G02 XP60.0 YP20.0 R50.0 F300.0 ;
G91 G02 XP60.0 YP20.0 R–50.0 F300.
G01- Linear interpolation
G01- Linear interpolation
G01-Tools can move along a line
A tools move along a line to the specified position at the feedrate
specified in F.
The feedrate specified in F is effective until a new value is specified. It
need not be specified for each block.
The feedrate commanded by the F code is measured along the tool path.
If the F code is not commanded, the feedrate is regarded as zero.
The feedrate of each axis direction is as follows.
G01
เคลื่อนที่ไปยังตำแหน่งงาน หรือแกน x,y,z ตามคำสั่งค่า F(feed)
EXAMPLE:
G00 G90 XO YO ...................วิ่งด้วยความเร็วไปที่ X0 Y0 ของงาน
G00 Z5 ................................วิ่งด้วยความเร็วไปที่ Z5
G01 Z-5 F100 ......................เดินด้วย feed 100mm/นาที ไปที่ Z-5
G01 Z5 F500 ........................เดินด้วย feed 500mm/นาที ไปที่ Z5
G00 Z100 .............................วิ่งด้วยความเร็วไปที่ Z100
G91 G00 G28 Z0 X0 Y0 .........วิ่งด้วยความเร็วไปที่ X0 Y0 Z0 ของเครื่อง
G01-Tools can move along a line
A tools move along a line to the specified position at the feedrate
specified in F.
The feedrate specified in F is effective until a new value is specified. It
need not be specified for each block.
The feedrate commanded by the F code is measured along the tool path.
If the F code is not commanded, the feedrate is regarded as zero.
The feedrate of each axis direction is as follows.
G01
เคลื่อนที่ไปยังตำแหน่งงาน หรือแกน x,y,z ตามคำสั่งค่า F(feed)
EXAMPLE:
G00 G90 XO YO ...................วิ่งด้วยความเร็วไปที่ X0 Y0 ของงาน
G00 Z5 ................................วิ่งด้วยความเร็วไปที่ Z5
G01 Z-5 F100 ......................เดินด้วย feed 100mm/นาที ไปที่ Z-5
G01 Z5 F500 ........................เดินด้วย feed 500mm/นาที ไปที่ Z5
G00 Z100 .............................วิ่งด้วยความเร็วไปที่ Z100
G91 G00 G28 Z0 X0 Y0 .........วิ่งด้วยความเร็วไปที่ X0 Y0 Z0 ของเครื่อง
วันศุกร์ที่ 29 มีนาคม พ.ศ. 2556
G code list -ไทย
G code list -ไทย
G code หน้าที่
G00 เดินเป็นเส้นตรง ควบคุมความเร็วตามRAPID
G01 เดินเป็นเส้นตรง ควบคุมความเร็วตามFEED OVERIDE
G02 เดินเป็นเส้นโค้ง ทิศทางตามเข็มนาฬิกา CW
G03 เดินเป็นเส้นโค้ง ทิศทางทวนเข็มนาฬิกา CCW
G04 หยุดทำงานชั่วขณะDwell, Exact stop
G09 หยุดตรงตำแหน่ง Exact stop
G10 ตั้งค่าข้อมูล Programmable data input
G17 การทำงานพร้อมกันของแกนXpYp plane selection
G18 การทำงานพร้อมกันของแกนZpXp plane selection
G19 การทำงานพร้อมกันของแกนYpZp plane selection
G20 การทำงานในระบบบนิ้ว Input in inch
G21 การทำงานในระบบบเมตริก Input in mm
G22 เปิดการทำงานฟังชั่น Stored stroke check function on
G23 ปิดการทำงานฟังชั่น Stored stroke check function off
G25 ปิดการทำงานฟังชั่น Spindle speed fluctuation detection off
G26 เปิดการทำงานฟังชั่น Spindle speed fluctuation detection on
G27 ตรวจสอบการเลื่อนกลับตำแหน่งอ้างอิง Reference position
G28 เลื่อนกลับตำแหน่งอ้างอิง Automatic return to reference position
G29 เลื่อนออกจากตำแหน่งอ้างอิง Automatic return from reference position
G30 เลื่อนกลับตำแหน่งอ้างอิงที่ 2nd, 3rd and 4th
G40 ยกเลิกคำสั่ง G41 G42
G41 ชดเชยค่ารํศมีของมีดตัดทางด้านซ้าย(มีดตัดอยู่ด้านซ้ายของทิศทางการเดิน)
G42 ชดเชยค่ารํศมีของมีดตัดทางด้านขวา(มีดตัดอยู่ด้านขวาของทิศทางการเดิน)
G43 ค่าความยาวของมีดตัดเป็นบวก
G44 ค่าความยาวของมีดตัดเป็นบวก
G45 เพิ่มค่ารัศมีของมีดตัดTool offset increase
G46 ลดค่ารัศมีของมีดตัดTool offset decrease
G47 เพิ่มค่ารัศมีของมีดตัด2เท่า Tool offset double increase
G48 ลดค่ารัศมีของมีดตัด2เท่า Tool offset double decrease
G49 ยกเลิกค่าความยาวของมีดตัดTool length
G50 Scaling cancel
G51 Scaling
G52 การตั้งระบบ Local coordinate system setting
G53 เลือกMachine coordinate system selection
G54 ค่า X0 Y0 Z0 ของงานตัวที่1
G55 ค่า X0 Y0 Z0 ของงานตัวที่2
G56 ค่า X0 Y0 Z0 ของงานตัวที่3
G57 ค่า X0 Y0 Z0 ของงานตัวที่4
G58 ค่า X0 Y0 Z0 ของงานตัวที่5
G59 ค่า X0 Y0 Z0 ของงานตัวที่6
G61 โหมดหยุดตรงตำแหน่งExact stop mode
G62 โหมดเดินมุมAutomatic corner override
G65 เรียกมาโครโปรแกรม Macro call
G67 ยกเลิกคำสั่งมาโครโปรแกรมMacro modal call cancel
G73 การเจาะแบบ Peck drilling cycle
G74 การทำเกลียวCounter tapping cycle
G76 การคว้านละเอียดFine boring cycle
G80 ยกเลิกคำสั่งCanned cycle cancel
G81 การเจาะDrilling cycle, spot boring cycle
G82 การเจาะDrilling cycle or counter boring cycle
G83 การเจาะPeck drilling cycle
G84 การทำเกลียวTapping cycle
G85 การใช้ดอกรีมเมอร์Boring cycle
G86 การคว้านBoring cycle
G87 การคว้านBack boring cycle
G88 การคว้านBoring cycle
G89 การคว้านBoring cycle
G90 คำสั่งโดยคิดจากจุดอ้างอิงAbsolute command
G91 คำสั่งโดยคิดจากจุดที่อยู่ครั้งสุดท้าย Increment command
G92 เปลี่ยนระบบ coordinate system or clamp at maximum spindle speed
G94 ฟีดต่อนาที Feed per minute
G95 ฟีดต่อรอบ Feed per rotation
G98 การเลื่อนกลับสู่ตำแหน่ง Z+ ตัวสุดท้าย
G99 การเลื่อนกลับสู่ตำแหน่ง R
G code หน้าที่
G00 เดินเป็นเส้นตรง ควบคุมความเร็วตามRAPID
G01 เดินเป็นเส้นตรง ควบคุมความเร็วตามFEED OVERIDE
G02 เดินเป็นเส้นโค้ง ทิศทางตามเข็มนาฬิกา CW
G03 เดินเป็นเส้นโค้ง ทิศทางทวนเข็มนาฬิกา CCW
G04 หยุดทำงานชั่วขณะDwell, Exact stop
G09 หยุดตรงตำแหน่ง Exact stop
G10 ตั้งค่าข้อมูล Programmable data input
G17 การทำงานพร้อมกันของแกนXpYp plane selection
G18 การทำงานพร้อมกันของแกนZpXp plane selection
G19 การทำงานพร้อมกันของแกนYpZp plane selection
G20 การทำงานในระบบบนิ้ว Input in inch
G21 การทำงานในระบบบเมตริก Input in mm
G22 เปิดการทำงานฟังชั่น Stored stroke check function on
G23 ปิดการทำงานฟังชั่น Stored stroke check function off
G25 ปิดการทำงานฟังชั่น Spindle speed fluctuation detection off
G26 เปิดการทำงานฟังชั่น Spindle speed fluctuation detection on
G27 ตรวจสอบการเลื่อนกลับตำแหน่งอ้างอิง Reference position
G28 เลื่อนกลับตำแหน่งอ้างอิง Automatic return to reference position
G29 เลื่อนออกจากตำแหน่งอ้างอิง Automatic return from reference position
G30 เลื่อนกลับตำแหน่งอ้างอิงที่ 2nd, 3rd and 4th
G40 ยกเลิกคำสั่ง G41 G42
G41 ชดเชยค่ารํศมีของมีดตัดทางด้านซ้าย(มีดตัดอยู่ด้านซ้ายของทิศทางการเดิน)
G42 ชดเชยค่ารํศมีของมีดตัดทางด้านขวา(มีดตัดอยู่ด้านขวาของทิศทางการเดิน)
G43 ค่าความยาวของมีดตัดเป็นบวก
G44 ค่าความยาวของมีดตัดเป็นบวก
G45 เพิ่มค่ารัศมีของมีดตัดTool offset increase
G46 ลดค่ารัศมีของมีดตัดTool offset decrease
G47 เพิ่มค่ารัศมีของมีดตัด2เท่า Tool offset double increase
G48 ลดค่ารัศมีของมีดตัด2เท่า Tool offset double decrease
G49 ยกเลิกค่าความยาวของมีดตัดTool length
G50 Scaling cancel
G51 Scaling
G52 การตั้งระบบ Local coordinate system setting
G53 เลือกMachine coordinate system selection
G54 ค่า X0 Y0 Z0 ของงานตัวที่1
G55 ค่า X0 Y0 Z0 ของงานตัวที่2
G56 ค่า X0 Y0 Z0 ของงานตัวที่3
G57 ค่า X0 Y0 Z0 ของงานตัวที่4
G58 ค่า X0 Y0 Z0 ของงานตัวที่5
G59 ค่า X0 Y0 Z0 ของงานตัวที่6
G61 โหมดหยุดตรงตำแหน่งExact stop mode
G62 โหมดเดินมุมAutomatic corner override
G65 เรียกมาโครโปรแกรม Macro call
G67 ยกเลิกคำสั่งมาโครโปรแกรมMacro modal call cancel
G73 การเจาะแบบ Peck drilling cycle
G74 การทำเกลียวCounter tapping cycle
G76 การคว้านละเอียดFine boring cycle
G80 ยกเลิกคำสั่งCanned cycle cancel
G81 การเจาะDrilling cycle, spot boring cycle
G82 การเจาะDrilling cycle or counter boring cycle
G83 การเจาะPeck drilling cycle
G84 การทำเกลียวTapping cycle
G85 การใช้ดอกรีมเมอร์Boring cycle
G86 การคว้านBoring cycle
G87 การคว้านBack boring cycle
G88 การคว้านBoring cycle
G89 การคว้านBoring cycle
G90 คำสั่งโดยคิดจากจุดอ้างอิงAbsolute command
G91 คำสั่งโดยคิดจากจุดที่อยู่ครั้งสุดท้าย Increment command
G92 เปลี่ยนระบบ coordinate system or clamp at maximum spindle speed
G94 ฟีดต่อนาที Feed per minute
G95 ฟีดต่อรอบ Feed per rotation
G98 การเลื่อนกลับสู่ตำแหน่ง Z+ ตัวสุดท้าย
G99 การเลื่อนกลับสู่ตำแหน่ง R
G00- Positioning
G00- Positioning
The G00 command moves a tool to the position in the workpiece system
specified with an absolute or an incremental command at a rapid traverse rate.
In the absolute command, coordinate value of the end point is programmed.
In the incremental command the distance the tool moves is programmed.
G00
เคลื่อนที่ไปยังตำแหน่งงาน หรือแกน x,y,zที่ตำแหน่งzero ด้วยความเร็วตามค่า rapid x25 - x100%
EXAMPLE:
G00 G90 XO YO ...............วิ่งด้วยความเร็วไปที่ X0 Y0 ของงาน
G00 Z5 ............................วิ่งด้วยความเร็วไปที่ Z5
G01 Z-5 F100 ...................เดินด้วย feed100mm/นาทีไปที่ Z-5
Z5 ....................................เดินด้วย feed 100mm/นาที ไปที่ Z5
G00 Z100 .........................วิ่งด้วยความเร็วไปที่ Z100
G91 G00 G28 Z0 X0 Y0 ....วิ่งด้วยความเร็วไปที่ X0 Y0 Z0 ของเครื่อง
The G00 command moves a tool to the position in the workpiece system
specified with an absolute or an incremental command at a rapid traverse rate.
In the absolute command, coordinate value of the end point is programmed.
In the incremental command the distance the tool moves is programmed.
G00
เคลื่อนที่ไปยังตำแหน่งงาน หรือแกน x,y,zที่ตำแหน่งzero ด้วยความเร็วตามค่า rapid x25 - x100%
EXAMPLE:
G00 G90 XO YO ...............วิ่งด้วยความเร็วไปที่ X0 Y0 ของงาน
G00 Z5 ............................วิ่งด้วยความเร็วไปที่ Z5
G01 Z-5 F100 ...................เดินด้วย feed100mm/นาทีไปที่ Z-5
Z5 ....................................เดินด้วย feed 100mm/นาที ไปที่ Z5
G00 Z100 .........................วิ่งด้วยความเร็วไปที่ Z100
G91 G00 G28 Z0 X0 Y0 ....วิ่งด้วยความเร็วไปที่ X0 Y0 Z0 ของเครื่อง
วันศุกร์ที่ 7 กันยายน พ.ศ. 2555
M CODE
M CODE LIST
command Description
M00 ProgramStop หยุดการทำงานของโปรแกรม
M01 Optional ProgramStop หยุดการทำงานของเครื่องจักร
M02 End-of-Program จบการทำงานโปรแกรม
M03 Spindle Start Forward หัวหมุนตามเข็มนาฬิกา
M04 Spindle Start Reverse หัวหมุนทวนเข็มนาฬิกา
M05 Spindle Stop หัวหยุดหมุน
M06 Run Tool Change Cycle , เปลี่ยนทูลM6 Txx
M07 Thru Spindle
M08 Coolant ON- Flood Colant เปิดน้ำหล่อเย็น
M09 Coolant OFF ปิดน้ำหล่อเย็น
M11 Set Tool Carousel position to 1(ATCTool Changer ONLY)
M19 cycle positioning(Not for spindle orientation) หัวอยู่ในตำแหน่งเปลี่ยนทูล
M20 Does nothing Standard.
M22 Chip Conveyor Toggle ON/OFF option
M29 Rigid Tap M29 Sxxxx in block prior to G84
M30 End-of-Program จบการทำงานโปรแกรม
M41 LowGear Select
M42 High Gear Select
M48 100%Spindle Speed Override Forced
M49 Released
M60 AAxis Brake ON
M61 AAxis Brake OFF
M62 B Axis Brake ON
M63 B Axis Brake OFF
M64 M64/65 Output ON
M65 M64/65 Output OFF
M66 M66/67 Output ON, ChipConveyor ON
M67 M66/67 Output OFF, ChipConveyor ON
M68 M68/69 Output ON, Wash Down ON
M69 M68/69 Output OFF, Wash Down OFF
M78 M78/79 Output ON, Cooled spindle ON(2016 &3016L)
M79 M78/79 Output OFF, Cooled spindle OFF(2016 &3016L)
M80 MIDACO Pallet Changer 2 When the machine has MIDACO pallet option
M85 AAxis Rotary Table Enable
M86 AAxis Rotary Table Disable
M87 B Axis Rotary Table Enable
M88 B Axis Rotary Table Disable
M98 Sub-ProgramCall เรียก subโปรแกรม
M99 Sub ProgramEnd จบ subโปรแกรม
command Description
M00 ProgramStop หยุดการทำงานของโปรแกรม
M01 Optional ProgramStop หยุดการทำงานของเครื่องจักร
M02 End-of-Program จบการทำงานโปรแกรม
M03 Spindle Start Forward หัวหมุนตามเข็มนาฬิกา
M04 Spindle Start Reverse หัวหมุนทวนเข็มนาฬิกา
M05 Spindle Stop หัวหยุดหมุน
M06 Run Tool Change Cycle , เปลี่ยนทูลM6 Txx
M07 Thru Spindle
M08 Coolant ON- Flood Colant เปิดน้ำหล่อเย็น
M09 Coolant OFF ปิดน้ำหล่อเย็น
M11 Set Tool Carousel position to 1(ATCTool Changer ONLY)
M19 cycle positioning(Not for spindle orientation) หัวอยู่ในตำแหน่งเปลี่ยนทูล
M20 Does nothing Standard.
M22 Chip Conveyor Toggle ON/OFF option
M29 Rigid Tap M29 Sxxxx in block prior to G84
M30 End-of-Program จบการทำงานโปรแกรม
M41 LowGear Select
M42 High Gear Select
M48 100%Spindle Speed Override Forced
M49 Released
M60 AAxis Brake ON
M61 AAxis Brake OFF
M62 B Axis Brake ON
M63 B Axis Brake OFF
M64 M64/65 Output ON
M65 M64/65 Output OFF
M66 M66/67 Output ON, ChipConveyor ON
M67 M66/67 Output OFF, ChipConveyor ON
M68 M68/69 Output ON, Wash Down ON
M69 M68/69 Output OFF, Wash Down OFF
M78 M78/79 Output ON, Cooled spindle ON(2016 &3016L)
M79 M78/79 Output OFF, Cooled spindle OFF(2016 &3016L)
M80 MIDACO Pallet Changer 2 When the machine has MIDACO pallet option
M85 AAxis Rotary Table Enable
M86 AAxis Rotary Table Disable
M87 B Axis Rotary Table Enable
M88 B Axis Rotary Table Disable
M98 Sub-ProgramCall เรียก subโปรแกรม
M99 Sub ProgramEnd จบ subโปรแกรม
G code
G code list
G code Function
G00 Positioning
G01 Linear interpolation
G02 Circular interpolation/Helical interpolation CW
G03 Circular interpolation/Helical interpolation CCW
G04 Dwell, Exact stop
G05 High speed cycle machining
G06.2 NURBS interpolation
G07 Hypothetical axis interpolation
G08 Advanced prevew control
G09 Exact stop
G10 Programmable data input
G11 Programmable data input mode cancel
G12.1 Polar coordinate interpolation mode
G13.1 Polar coordinate interpolation cancel mode
G15 Polar coordinates command cancel
G16 Polar coordinates command
G17 XpYp plane selection Xp: X axis or its parallel axis
G18 ZpXp plane selection Yp: Y axis or its parallel axis
G19 YpZp plane selection Zp: Z axis or its parallel axis
G20 Input in inch
G21 Input in mm
G22 Stored stroke check function on
G23 Stored stroke check function off
G25 Spindle speed fluctuation detection off
G26 Spindle speed fluctuation detection on
G27 Reference position return check
G28 Automatic return to reference position
G29 Automatic return from reference position
G30 2nd, 3rd and 4th reference position return
G31 Skip function
G33 Thread cutting
G37 Automatic tool length measurment
G39 Corner offset circular interpolation
G40 Cutter compensation cancel/three dimensional tool compensation cancel
G41 Cutter compensation left/three dimensional tool compensation
G42 Cutter compensation right
G43 Tool length compensation direction
G44 Tool length compensation direction
G45 Tool offset increase
G46 Tool offset decrease
G47 Tool offset double increase
G48 Tool offset double decrease
G49 Tool length compensation cancel
G50 Scaling cancel
G51 Scaling
G52 Local coordinate system setting
G53 Machine coordinate system selection
G54 Workpiece coordinate system 1 selection
G54.1 Additional workpiece coordinate system selection
G54.2 Rotary table dynamic fixture offset
G55 Workpiece coordinate system 2 selection
G56 Workpiece coordinate system 3 selection
G57 Workpiece coordinate system 4 selection
G58 Workpiece coordinate system 5 selection
G59 Workpiece coordinate system 6 selection
G60 Single direction positioning
G61 Exact stop mode
G62 Automatic corner override
G63 Tapping mode
G64 Cutting mode
G65 Macro call
G66 Macro modal call
G67 Macro modal call cancel
G68 Coordinate rotation/threeญdimensional coordinate conversion
G69 Coordinate rotation cancel/threeญdimensional coordinate conversion cancel
G73 Peck drilling cycle
G74 Counter tapping cycle
G75 Plunge grinding cycle (for grinding machine)
G76 Fine boring cycle
G77 Direct constantญdimension plunge grinding cycle(for grinding machine)
G78 Continuousญfeed surface grinding cycle(for grinding machine)
G79 Intermittentญfeed surface grinding cycle(for grinding machine)
G80 Canned cycle cancel/external operation function cancel
G81 Drilling cycle, spot boring cycle or external operation function
G82 Drilling cycle or counter boring cycle
G83 Peck drilling cycle
G84 Tapping cycle
G85 Boring cycle
G86 Boring cycle
G87 Back boring cycle
G88 Boring cycle
G89 Boring cycle
G90 Absolute command
G91 Increment command
G92 Setting for work coordinate system or clamp at maximum spindle speed
G94 Feed per minute
G95 Feed per rotation
G96 Constant surface speed control
G97 Constant surface speed control cancel
G98 Return to initial point in canned cycle
G99 Return to R point in canned cycle
G code Function
G00 Positioning
G01 Linear interpolation
G02 Circular interpolation/Helical interpolation CW
G03 Circular interpolation/Helical interpolation CCW
G04 Dwell, Exact stop
G05 High speed cycle machining
G06.2 NURBS interpolation
G07 Hypothetical axis interpolation
G08 Advanced prevew control
G09 Exact stop
G10 Programmable data input
G11 Programmable data input mode cancel
G12.1 Polar coordinate interpolation mode
G13.1 Polar coordinate interpolation cancel mode
G15 Polar coordinates command cancel
G16 Polar coordinates command
G17 XpYp plane selection Xp: X axis or its parallel axis
G18 ZpXp plane selection Yp: Y axis or its parallel axis
G19 YpZp plane selection Zp: Z axis or its parallel axis
G20 Input in inch
G21 Input in mm
G22 Stored stroke check function on
G23 Stored stroke check function off
G25 Spindle speed fluctuation detection off
G26 Spindle speed fluctuation detection on
G27 Reference position return check
G28 Automatic return to reference position
G29 Automatic return from reference position
G30 2nd, 3rd and 4th reference position return
G31 Skip function
G33 Thread cutting
G37 Automatic tool length measurment
G39 Corner offset circular interpolation
G40 Cutter compensation cancel/three dimensional tool compensation cancel
G41 Cutter compensation left/three dimensional tool compensation
G42 Cutter compensation right
G43 Tool length compensation direction
G44 Tool length compensation direction
G45 Tool offset increase
G46 Tool offset decrease
G47 Tool offset double increase
G48 Tool offset double decrease
G49 Tool length compensation cancel
G50 Scaling cancel
G51 Scaling
G52 Local coordinate system setting
G53 Machine coordinate system selection
G54 Workpiece coordinate system 1 selection
G54.1 Additional workpiece coordinate system selection
G54.2 Rotary table dynamic fixture offset
G55 Workpiece coordinate system 2 selection
G56 Workpiece coordinate system 3 selection
G57 Workpiece coordinate system 4 selection
G58 Workpiece coordinate system 5 selection
G59 Workpiece coordinate system 6 selection
G60 Single direction positioning
G61 Exact stop mode
G62 Automatic corner override
G63 Tapping mode
G64 Cutting mode
G65 Macro call
G66 Macro modal call
G67 Macro modal call cancel
G68 Coordinate rotation/threeญdimensional coordinate conversion
G69 Coordinate rotation cancel/threeญdimensional coordinate conversion cancel
G73 Peck drilling cycle
G74 Counter tapping cycle
G75 Plunge grinding cycle (for grinding machine)
G76 Fine boring cycle
G77 Direct constantญdimension plunge grinding cycle(for grinding machine)
G78 Continuousญfeed surface grinding cycle(for grinding machine)
G79 Intermittentญfeed surface grinding cycle(for grinding machine)
G80 Canned cycle cancel/external operation function cancel
G81 Drilling cycle, spot boring cycle or external operation function
G82 Drilling cycle or counter boring cycle
G83 Peck drilling cycle
G84 Tapping cycle
G85 Boring cycle
G86 Boring cycle
G87 Back boring cycle
G88 Boring cycle
G89 Boring cycle
G90 Absolute command
G91 Increment command
G92 Setting for work coordinate system or clamp at maximum spindle speed
G94 Feed per minute
G95 Feed per rotation
G96 Constant surface speed control
G97 Constant surface speed control cancel
G98 Return to initial point in canned cycle
G99 Return to R point in canned cycle
วันพุธที่ 1 ธันวาคม พ.ศ. 2553
กลอนฮาๆๆอย่าคิดมาก
กลอนฮาๆๆอย่าคิดมาก(555555)
จิตรกรใช้อารมณ์ผสมสี นักดนตรีใช้อารมณ์ผสมเสียง
นักร้องใช้อารมณ์ผสมสำเนียง นอนบนเตียงใช้อารมณ์ผสมพันธุ์
สามีคือเป้าหมาย ผู้ชายคือทางผ่าน
แพศยาคือนิพพาน ขึ้นคานคือตายทั้งเป็น
รักแรกคือฟันน้ำนม รักระบมคือฟันหลุด
รักที่สุดคือฟันเธอ รักเสมอคือเธอหั้ยฟัน
ชายแรกคือความรู้ ชายชู้คือวิชา
ชายต่อมาคือประสบการณ์ ชายตูดบานคือกระเทย
อยากเป็นตุ๊กตาหมีให้เธอกอด อยากเป็นทามาก็อตให้เธอเลี้ยง
อยากเป็นทูตสวรรค์ข้างๆเตียง อยากเป็นนกเอี้ยงคอยเลี้ยงเธอ
อิจฉาเครื่องบินที่อยู่ใกล้แอร์พอร์ท อิจฉาปรอทที่อยู่ใกล้คนไข้
อิจฉาเส้นเลือดใหญ่ที่อยู่ใกล้หัวใจ อิจฉากางเกงในที่อยู่ใกล้เธอ
src="http://pagead2.googlesyndication.com/pagead/show_ads.js">
ย า ม เ ธ อ ยิ้ ม
ยามเธอยิ้ม ปานอีแร้งแย่งหมาเน่า
ยามเธอเศร้า ช่างละม้ายคล้ายกับผี
ยามเธอยิ้ม ช่างยั่วยวนกวนตีนดี
ยิ้มอีกทีเตะคอพับหลับคาตีน
ท้ อ ง ป่ อ ง
พอหน้าท้อง ของแม่ เริ่มป่องออก
พ่อก็บอก อยากให้ลูก เป็นดอกเตอร์
ย่าก็อยาก ให้หลานเป็น นายอำเภอ
แต่ต้องเก้อ หมอบอกแม่ แค่ลงพุง
น อ น กั บ ศ พ
เมื่อคืนฝันสยองตีสองกว่า
ฝันไปว่านอนซบกับศพผี
นอนขึ้นอืดค้างตายมาหลายปี
เหมือนปิศาจอเวจีที่น่ากลัว
เหม็นซากศพ อบอวลไปทั่วห้อง
ไม่กล้ามองต้องคู้คด นอนหดหัว
ตกใจตื่นขนลุกซู่ ดูรอบตัว
เห็นชัวร์ ๆ เมียนอนตด สลดใจ
บ ว ก เ ล ข
สามสิบหกคืออกอันเซ็กซี่
ยี่สิบสี่คือเอวองค์โฉมเฉลา
สามสิบห้าคือบั้นท้ายร้ายไม่เบา
รวมกันเข้าเก้าสิบหกอายุเธอ
ค ว า ม รั ก ข อ ง โ ป ร แ ก ร ม เ ม อ ร์
เอา array มาเก็บความรัก
เอา buffer มาพักใจไว้
เอา struct มาใส่ความห่วงใย
แล้ว save เก็บไว้ในหัวใจเธอ
complie ความปรารถนาดี
ที่ execute ไว้เสมอ
ยามใดที่ interrupt แล้วพบเจอ อยากจะ copy หน้าเธอไว้ทุกมุม
ls ดูความจริงใจ
ftp ความคิดถึงไปทั่วกลุ่ม
declare ความห่วงหาให้ครอบคลุม
แล้ว click ปุ่มเพื่อส่งความหวังดี
del ความบาดหมางของสองใจ network เชื่อมใยใจที่ล้นปรี่
ให้ ram เก็บความรู้สึกที่มี
ใช้ pointer ชี้สายสัมพันธ์ เก็บค่าความสุขลง file
แล้ว move ย้ายค่าความโศกศัลย์ ทิ้งไปใน bin โดยพลัน
เหลือ quota ไว้แค่ฉันกะเธอ
ย อ ม
ฉันรักเธอเพ้อหาจนหน้าแห้ง
สุดแสยงสุดสยิวหิวกระหาย
แม้นอกหักรักนี้ขี้แตกตาย
ฉันยอมอายตายคาขี้ดีกว่าเอย
เ ส ริ ม
มีใจ
เห็นใจ
ดูใจ
ถอดใจ
คืนใจ
ตัดใจ
ในที่สุดก็ ไร้ใจ (อนัตตา)
จิตรกรใช้อารมณ์ผสมสี นักดนตรีใช้อารมณ์ผสมเสียง
นักร้องใช้อารมณ์ผสมสำเนียง นอนบนเตียงใช้อารมณ์ผสมพันธุ์
สามีคือเป้าหมาย ผู้ชายคือทางผ่าน
แพศยาคือนิพพาน ขึ้นคานคือตายทั้งเป็น
รักแรกคือฟันน้ำนม รักระบมคือฟันหลุด
รักที่สุดคือฟันเธอ รักเสมอคือเธอหั้ยฟัน
ชายแรกคือความรู้ ชายชู้คือวิชา
ชายต่อมาคือประสบการณ์ ชายตูดบานคือกระเทย
อยากเป็นตุ๊กตาหมีให้เธอกอด อยากเป็นทามาก็อตให้เธอเลี้ยง
อยากเป็นทูตสวรรค์ข้างๆเตียง อยากเป็นนกเอี้ยงคอยเลี้ยงเธอ
อิจฉาเครื่องบินที่อยู่ใกล้แอร์พอร์ท อิจฉาปรอทที่อยู่ใกล้คนไข้
อิจฉาเส้นเลือดใหญ่ที่อยู่ใกล้หัวใจ อิจฉากางเกงในที่อยู่ใกล้เธอ
src="http://pagead2.googlesyndication.com/pagead/show_ads.js">
ย า ม เ ธ อ ยิ้ ม
ยามเธอยิ้ม ปานอีแร้งแย่งหมาเน่า
ยามเธอเศร้า ช่างละม้ายคล้ายกับผี
ยามเธอยิ้ม ช่างยั่วยวนกวนตีนดี
ยิ้มอีกทีเตะคอพับหลับคาตีน
ท้ อ ง ป่ อ ง
พอหน้าท้อง ของแม่ เริ่มป่องออก
พ่อก็บอก อยากให้ลูก เป็นดอกเตอร์
ย่าก็อยาก ให้หลานเป็น นายอำเภอ
แต่ต้องเก้อ หมอบอกแม่ แค่ลงพุง
น อ น กั บ ศ พ
เมื่อคืนฝันสยองตีสองกว่า
ฝันไปว่านอนซบกับศพผี
นอนขึ้นอืดค้างตายมาหลายปี
เหมือนปิศาจอเวจีที่น่ากลัว
เหม็นซากศพ อบอวลไปทั่วห้อง
ไม่กล้ามองต้องคู้คด นอนหดหัว
ตกใจตื่นขนลุกซู่ ดูรอบตัว
เห็นชัวร์ ๆ เมียนอนตด สลดใจ
บ ว ก เ ล ข
สามสิบหกคืออกอันเซ็กซี่
ยี่สิบสี่คือเอวองค์โฉมเฉลา
สามสิบห้าคือบั้นท้ายร้ายไม่เบา
รวมกันเข้าเก้าสิบหกอายุเธอ
ค ว า ม รั ก ข อ ง โ ป ร แ ก ร ม เ ม อ ร์
เอา array มาเก็บความรัก
เอา buffer มาพักใจไว้
เอา struct มาใส่ความห่วงใย
แล้ว save เก็บไว้ในหัวใจเธอ
complie ความปรารถนาดี
ที่ execute ไว้เสมอ
ยามใดที่ interrupt แล้วพบเจอ อยากจะ copy หน้าเธอไว้ทุกมุม
ls ดูความจริงใจ
ftp ความคิดถึงไปทั่วกลุ่ม
declare ความห่วงหาให้ครอบคลุม
แล้ว click ปุ่มเพื่อส่งความหวังดี
del ความบาดหมางของสองใจ network เชื่อมใยใจที่ล้นปรี่
ให้ ram เก็บความรู้สึกที่มี
ใช้ pointer ชี้สายสัมพันธ์ เก็บค่าความสุขลง file
แล้ว move ย้ายค่าความโศกศัลย์ ทิ้งไปใน bin โดยพลัน
เหลือ quota ไว้แค่ฉันกะเธอ
ย อ ม
ฉันรักเธอเพ้อหาจนหน้าแห้ง
สุดแสยงสุดสยิวหิวกระหาย
แม้นอกหักรักนี้ขี้แตกตาย
ฉันยอมอายตายคาขี้ดีกว่าเอย
เ ส ริ ม
มีใจ
เห็นใจ
ดูใจ
ถอดใจ
คืนใจ
ตัดใจ
ในที่สุดก็ ไร้ใจ (อนัตตา)
รายชื่อโรงงาน
รายชื่อโรงงานผลิตชิ้นส่วนยานยนต์,อีเล็กทรอนิกส์,แม่พิมพ์,
ชิ้นส่วนต่างๆจากงานแมชชีน,และอื่นๆ
สำหรับการทำตลาด คัตติ้งทูล(cuttingtools) เม็ดมีด(insert)
น้ำมันหล่อเย็น(coolant) และอื่นๆ
กว่าสามหมื่นรายชื่อโรงงาน ครอบครุม พระนครศรีอยุธยา,ปทุมธานี,
สมุทรปราการ,ขอนแก่น,นครราชสีมา
สระบุรี,นนทบุรี,นิคมลำพูน ,อ่างทอง และเขตอุตสาหกรรมอื่นๆ
และนามบัตรโรงงานในเขตนิคมนวนคร,นิคมโรจนะ,นิคมไฮเทค,
นิคมบางปะอิน,นิคมสหรัตนนคร,นิคม sil
สำหรับการทำตลาด คัตติ้งทูล(cuttingtools) เม็ดมีด(insert)
น้ำมันหล่อเย็น(coolant)โดยเฉพาะ
สนใจติดต่อ tt6499@gmail.com 089-7903309
สมัครสมาชิก:
บทความ (Atom)